简体中文
 English
 اللغة العربية
 Español
Why Welding Quality of Sanitary Stainless Steel Pipes Can Never Be Ignored
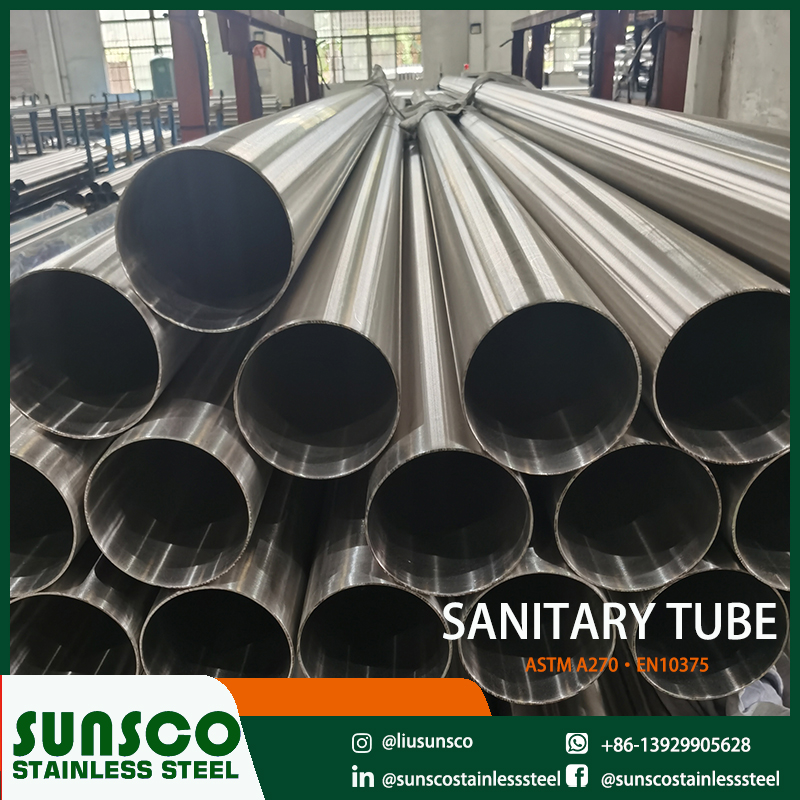
In high-purity industries such as biopharmaceuticals, food and beverage, fine chemicals, and semiconductor manufacturing, sanitary stainless steel tubing acts as the crucial "artery" for fluid transfer. Unlike standard industrial piping, sanitary systems carry materials that are highly prone to spoilage, expensive biological liquids, or ultra-pure process media.
Lack of Penetration: The backside of the weld fails to fuse completely, leaving a sharp, microscopic "V-shaped" crevice.
Over-penetration and Undercutting: Excessive weld metal protrudes inward, or the base metal burns away, creating uneven ridges.
Under a microscope, these pits and burrs act as a microscopic maze. As fluids pass through, they create turbulence and stagnant zones where product residue becomes trapped. This leads to the formation of a biofilm. Once established, a biofilm acts as a protective shield for bacteria, resisting standard chemical flushes and high-temperature steam, resulting in persistent microbial contamination of your product.
In the critical temperature range of 450°C to 850°C, carbon rapidly binds with chromium to form chromium carbides (Cr₂₃C₆) along the grain boundaries.
This depletes the surrounding matrix of free chromium, dropping its concentration below the critical 12% threshold required for corrosion resistance.
When the system processes fluids containing chlorides, mild acids, or caustic cleaning agents, the HAZ becomes highly susceptible to intergranular corrosion or pitting. Severe intergranular corrosion causes structural degradation from within, leading to sudden pinhole leaks, pipe bursts, and catastrophic batch contamination.
These discolored oxide scales are structurally loose, highly porous, iron-rich, and chromium-deficient. Over time, exposure to fluid friction and corrosive CIP chemicals breaks down this weak layer, converting it into red rust. In pharmaceutical Water for Injection (WFI) or purified water systems, red rust particles shed into the fluid stream, leading to instant batch rejection.
Regulatory Standards: The ASME BPE (Bioprocess Equipment) standard dictates stringent quantitative limits on sanitary weld profiles, misalignment (high-lo), weld width variation, convexity, concavity, and allowable heat tint levels.
Inspection Mandates: Industry regulations often mandate automated orbital welding over manual welding. Furthermore, facilities must perform 100% borescope inspections on interior welds, backed by comprehensive weld logs and radiographic testing (RT) records.
Substandard welding practices leave a digital paper trail of non-compliance. During 3Q validation (IQ/OQ/PQ) or regulatory audits by bodies like the US FDA or EMA, deficient borescope footage or incomplete weld logs will trigger major audit findings. This can halt factory commissioning, costing companies millions in delayed market entry.
-
[Company news] High quality supply of stainless steel pipe for ho......
2022-04-10
After years of development and innovation, the stainless steel pipe for household decoration has evolved from a single "slot body" to a "system" produ......
-
[Company news] Warmly celebrate the official launch of the fsunsc......
2005-07-19
Foshan Sunsco Technology Co.Ltd is located in Foshan City of China, focusing on stainless steel area for more than 12 years. With the support of the m......
-
[Industry dynamics] 304 stainless steel pipe market improves
2021-12-20
FSUNSCO Company operates a series of 304 stainless steel tubes all the year round. Stainless steel pipe, 304 stainless steel plate, 304 stainless stee......
-
[Industry dynamics] What can help us to quickly distinguish between 30......
2020-06-20
Many friends will worry when choosing stainless steel, this is because he can not distinguish between 304 and 201 stainless steel, how to quickly dist......