Unveiling Hidden Defects in Industrial Stainless Steel Pipes: Failure Mechanisms from Metallurgy to Application
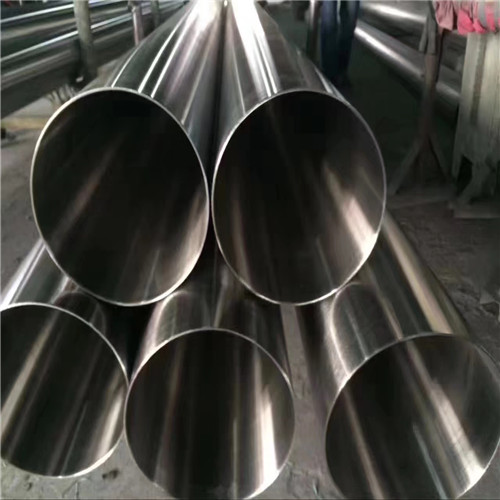
In modern fluid transportation, pressure vessels, and structural engineering, stainless steel pipes are widely relied upon for their superior corrosion resistance and mechanical strength. However, procurement managers and project engineers frequently encounter a baffling phenomenon: even when they purchase Grade 304 or 316L pipes that explicitly comply with ASTM or national standards, the piping network suffers from severe cracking, pitting, or weld leakage shortly after commissioning.
Most online articles simplify these catastrophic events by blaming them on "counterfeit materials" or "harsh operating environments." This article moves past those superficial narratives to explore the root causes of stainless steel pipe quality issues from the advanced perspectives of material metallurgy, residual manufacturing stress, and processing defects.
1. Genetic Defects at the Source: Chemical Composition & Non-Metallic Inclusions
Up to 70% of a finished stainless steel pipe’s ultimate quality is determined during the initial smelting and billet casting phase. Low-tier manufacturers cutting corners often introduce latent flaws right at the melting shop.
The Tug-of-War Between Carbon and Chromium: Intergranular Corrosion (IGC)
When stainless steel undergoes welding or operates at elevated temperatures (450°C to 850°C), excessive carbon within the steel matrix diffuses toward the grain boundaries. It binds with chromium to form chromium carbides (Cr₂₃C₆) that precipitate out. This creates a "chromium-depleted zone" along the grain boundaries where the local chromium level falls below the critical 11% passivity threshold. Under corrosive media, this triggers rapid Intergranular Corrosion (IGC). This is precisely why high-end industrial projects mandate strict carbon caps (e.g., the "L" in 316L stands for Low Carbon).
Non-Metallic Inclusions: The Initiation Sites for Pitting
In inadequate refining processes, incomplete deoxidation or desulfurization leaves a high volume of sulfides and silicates (non-metallic inclusions) trapped in the steel matrix. When the pipe's surface is exposed to aggressive chloride ions (Cl⁻), the interfaces between these inclusions and the steel matrix act as weak links where the passive film breaks down first. This leads to pitting corrosion, a localized, structural hazard that is highly destructive yet difficult to detect with the naked eye.
2. The Invisible Killers in Manufacturing: Residual Stress & Substandard Heat Treatment
Manufacturing a reliable industrial pipe involves far more than simply roll-forming a steel plate. It demands rigorous downstream thermo-mechanical control.
[Quality Control Chain of Stainless Steel Pipe Manufacturing]
Raw Plate Inspection ➔ Precision Welding ➔ Solution Annealing (Stress Relief) ➔ Eddy Current/UT NDT ➔ Pickling & Passivation
Residual Cold-Working Stress and Stress Corrosion Cracking (SCC)
During cold drawing or cold rolling, stainless steel pipes experience immense residual internal stress. If a manufacturer bypasses the crucial solution annealing stage to save on energy costs, these internal stresses remain locked within the tube walls. When exposed to specific environments (such as chloride-bearing solutions or high-temperature water) while under tensile loads, the pipe can suffer sudden Stress Corrosion Cracking (SCC) at stress levels far below its rated yield strength, causing catastrophic pipeline failures.
Incomplete Weld Seam Solid Solution Treatment
For welded stainless steel pipes, structural integrity relies entirely on the weld zone. If the welding heat input is poorly regulated, the weld and the Heat-Affected Zone (HAZ) will experience grain coarsening or a disproportionate ferrite-to-austenite ratio. Weld seams that do not undergo online bright solution annealing exhibit severely compromised mechanical properties and drastically lower corrosion resistance compared to the base metal.
3. Direct Mapping: Common Stainless Steel Pipe Quality Defects
To assist procurement teams and QC inspectors in field evaluations, the table below highlights common surface and internal defects found in industrial-grade pipelines:
| Defect Name | Visual Characteristics | Root Engineering Cause | Potential Operational Hazard |
|---|
| Internal Scratches / Scoring | Continuous or intermittent longitudinal grooves inside the bore | Damaged drawing dies, poor lubrication, or debris during cold drawing | Acts as a trap for stagnant media, initiating localized crevice corrosion |
| Lack of Fusion / Pinholes | Unfused gaps at the root of the weld, or micro-orifices | Insufficient welding current, excessive travel speed, or poor shielding gas coverage | Direct localized leakage or rupture under high-pressure fluid spikes |
| "Orange Peel" Surface | Microscopic surface roughness or wrinkling during bending/stretching | Excessively coarse grain size due to overheating or overholding during heat treatment | Reduces the structural fatigue life of the pipe under cyclic loading |
| Acid Spots / Over-Pickling | Dull grey, rough surface finish with visible structural etching | Imbalanced chemical ratios in the pickling bath or prolonged immersion times | Destroys the tight passive layer, accelerating oxidation and early rusting |
4. Engineering Framework to Eliminate Quality Risks
Project engineering teams can systematically screen out substandard steel pipes by enforcing a rigorous testing matrix before field deployment:
Mandate 100% Non-Destructive Testing (NDT): Ensure all industrial-grade pipes undergo Eddy Current Testing (ET) or Ultrasonic Testing (UT) to capture internal volumetric defects like micro-fissures and lack of weld fusion that bypass visual checks.
Enforce Hydrostatic & Pneumatic Proof Testing: For fluid-conveying lines, a high-pressure hydrostatic test remains the absolute standard to evaluate structural soundness and identify pinpoint leakages.
Validate Mill Test Certificates (MTC) with Field PMI: Do not rely solely on paperwork from unverified suppliers. Deploy portable X-ray Fluorescence (XRF) spectrometers for on-site Positive Material Identification (PMI) to guarantee that critical alloying elements like Nickel, Chromium, and Molybdenum are fully up to specification.
Conclusion
The structural integrity of a stainless steel pipe is rarely determined by its outer appearance. Fierce price competition often forces low-tier mills to compromise on hidden, energy-intensive processes like refining, solution annealing, and non-destructive testing. Partnering with premium manufacturers holding robust quality certifications (e.g., ISO 9001, PED) and executing rigorous receiving inspections is the only definitive way to secure long-term, risk-free industrial pipeline operations.


 简体中文
 English
 اللغة العربية
 Español